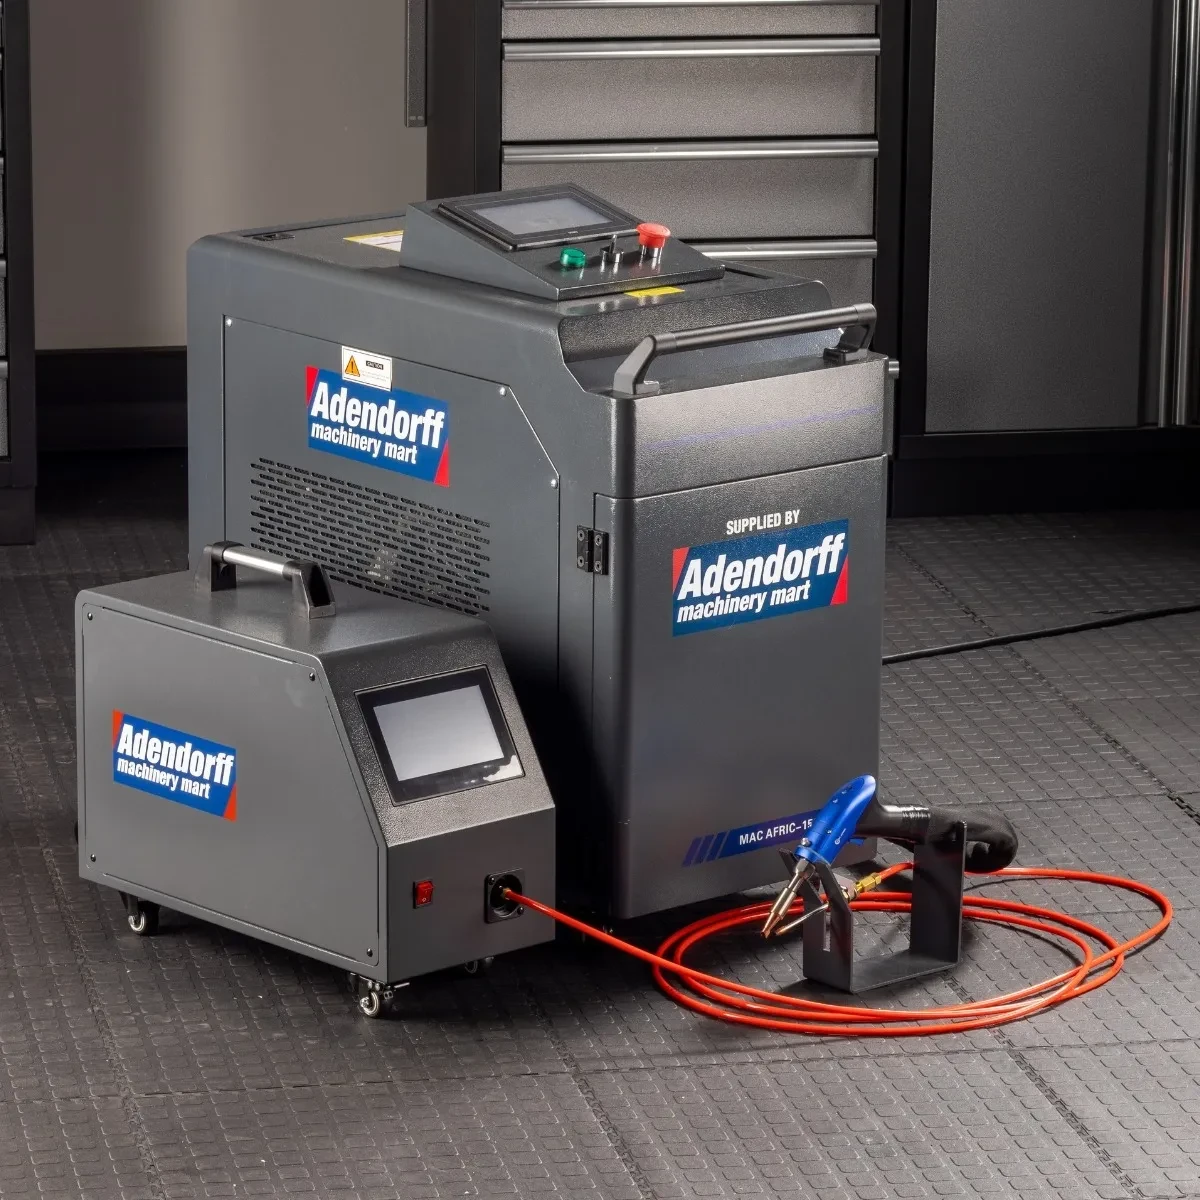
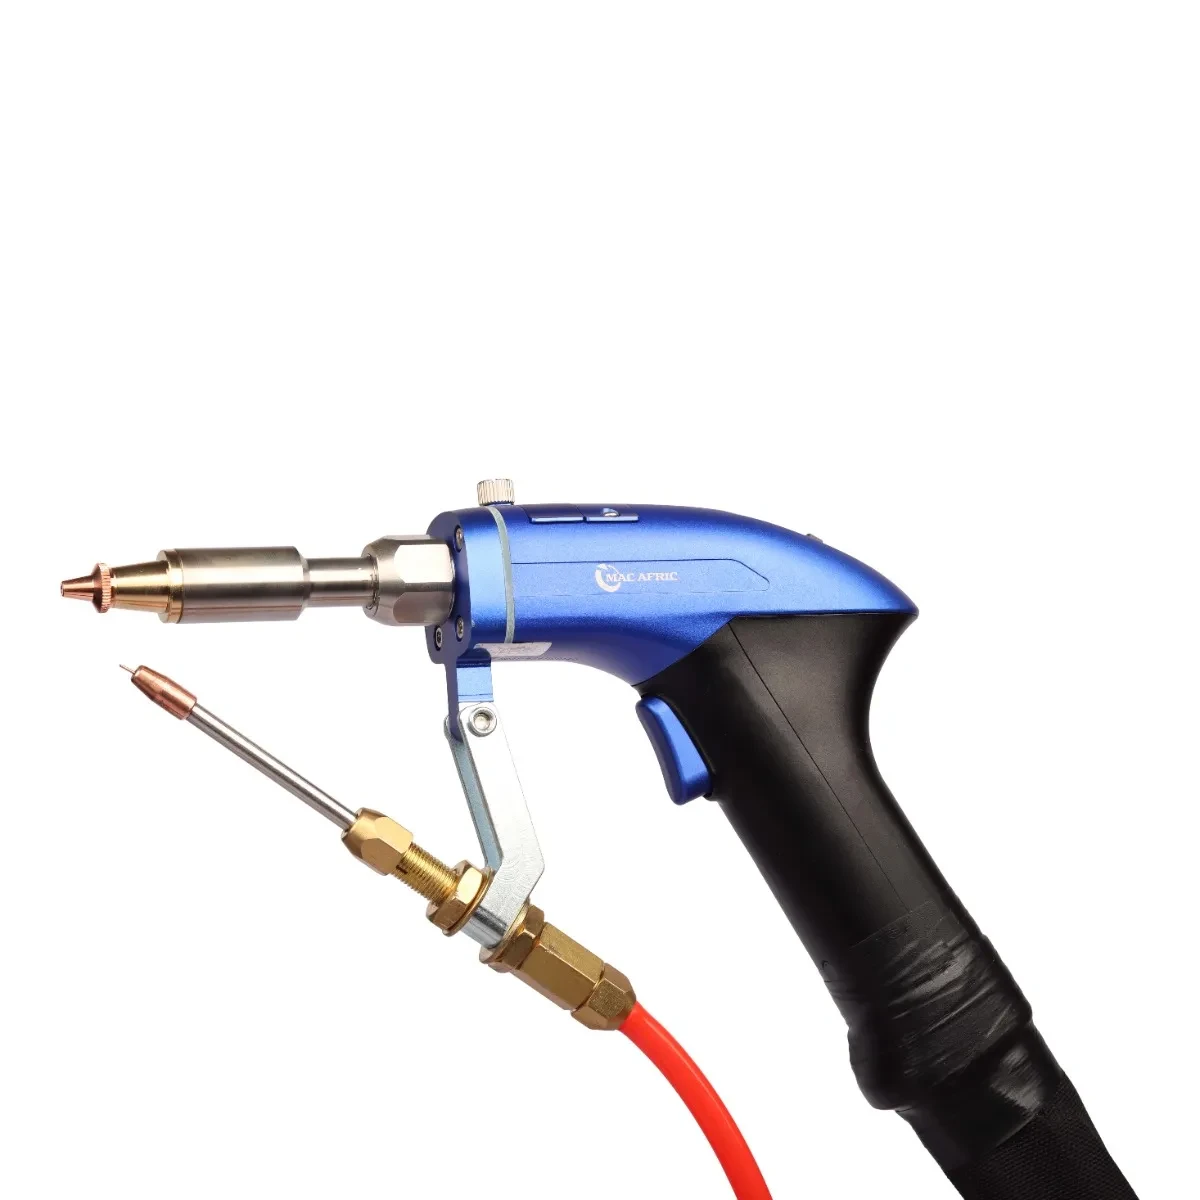
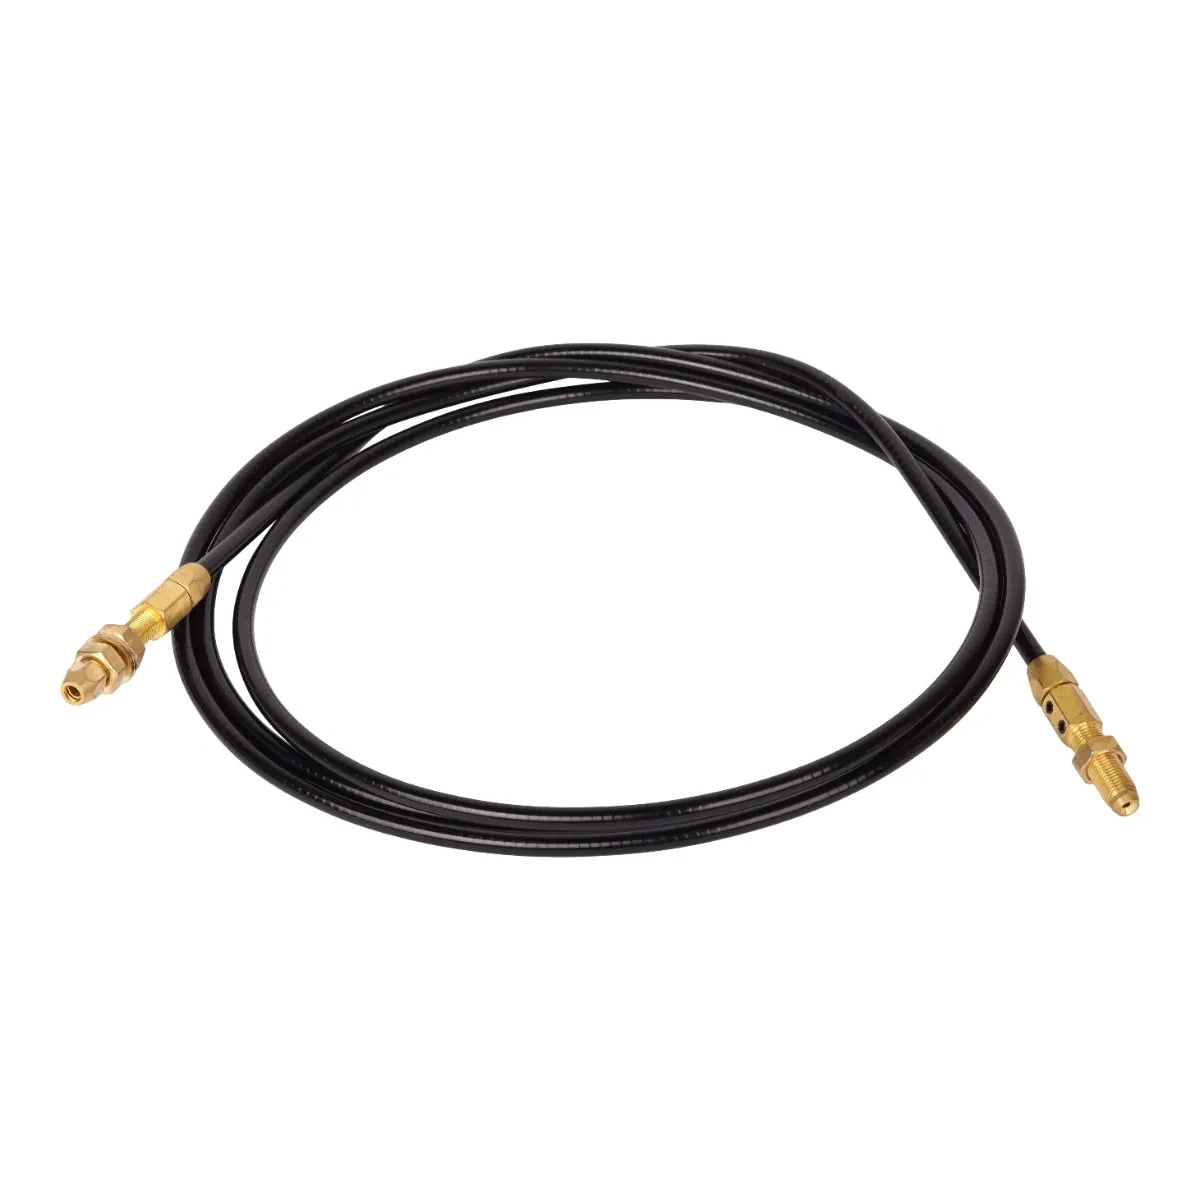
The Mac Afric Hand-Held Laser Welding Machine, 1500W , offers high-precision welding with a fiber length of 10M and a speed of up to 120mm/s. Ideal for industrial applications requiring strong, clean welds.
Technical Specifications
| FeatureSpecification |
|
| Laser Power | 1500 W+ |
| Laser Wavelength | 1080 ± 10 nm |
| Fiber Length | 10 m |
| Operate Mode | Continuous / Modulation |
| Welding Speed | 0 – 120 mm/s |
| Cooling System | Industrial Constant Temp Tank |
| Working Environment Temp Range | 10°C to 40°C |
| Working Environment Humidity | 70% Without Condensation |
| Welding Thickness | 0.5 – 4 mm |
| Welding Gap Requirements | 0.5 mm |
| Working Voltage | 220 V 50 Hz |
Key Features
- Supports continuous and modulated operation modes
- High energy efficiency up to 35%
- Welding speed up to 5x faster than traditional methods
- Welds carbon steel, stainless steel, aluminum, and galvanized steel
- Built-in safety interlock system with clamp activation
- Laser wavelength of 1080 ± 5 nm with fine beam quality
Safety Precautions
- Always wear full PPE including laser-rated eye protection
- Ensure 220V single-phase input supply
- Do not look directly at the laser beam
- Maintain coolant levels in water-cooled units
- Use dry, clean compressed air in plasma mode
- Ensure proper grounding of workpiece and machine
Troubleshooting Guide
| IssueLikely CauseSolution |
|
|
| Machine Does Not Power On | No mains power, blown fuse, faulty switch | Check supply, reset breaker, test switch |
| No Laser Output | Interlock not engaged, dirty lens, wrong settings | Check interlocks, clean lens, reset parameters |
| Weak or Unstable Arc | Low power, dirty workpiece, poor grounding | Increase power, clean metal, secure clamp |
| Plasma Torch Won’t Ignite | Low air pressure, worn tip, bad trigger | Ensure 4.5–6 bar pressure, replace parts, check trigger wiring |
| Excessive Dross (Plasma) | Wrong speed, worn tip, bad air pressure | Adjust speed, replace tip, reset pressure |
| Machine Overheating | Duty cycle exceeded, clogged vents | Let cool, observe duty cycle, clean vents |
Recommended Laser Welding Settings
| MaterialThicknessEWELDL150EWELDL200Notes |
|
|
|
|
| Mild Steel | 0.8–1.5 mm | 40–60% power | 50–70% power | Single pass, thin sheets |
| Mild Steel | 2–3 mm | 60–80% power | 70–90% power | Pre-clean surface |
| Stainless Steel | 1–2 mm | 50–70% power | 60–80% power | Pulsed mode recommended |
| Stainless Steel | 3–4 mm | 70–90% power | 80–100% power | Multi-pass if needed |
| Aluminium | 1–2 mm | 50–70% power | 60–80% power | Stable hand movement required |
| Aluminium | 3–4 mm | Near max | 80–100% power | Prefer EWELDL200 |
Recommended Plasma Cutting Settings
| MaterialThicknessEWELDL150EWELDL200Air PressureNotes |
|
|
|
|
|
| Mild Steel | 1–3 mm | 20–30 A | 25–35 A | 4.5 bar | Smooth sheet cutting |
| Mild Steel | 4–6 mm | 30–40 A | 40–50 A | 5.0 bar | Clean edges |
| Mild Steel | 8–10 mm | 40–50 A | 50–70 A | 5.5 bar | 150 at limit |
| Mild Steel | 12–16 mm | Not recommended | 70–90 A | 6.0 bar | Use EWELDL200 |
| Stainless Steel | 3–6 mm | 25–40 A | 40–60 A | 5.0 bar | Slower feed |
| Aluminium | 3–8 mm | 25–40 A | 40–60 A | 5.5 bar | Steady arc |
Quick Tips & Notes
- EWELDL150 is ideal for thinner material and light fabrication
- EWELDL200 offers higher output for thicker jobs and longer duty cycles
- Keep torch angle between 5–15° and maintain steady hand movement
- Clean work surfaces before every weld
- Replace consumables regularly for consistent results

 English
 English