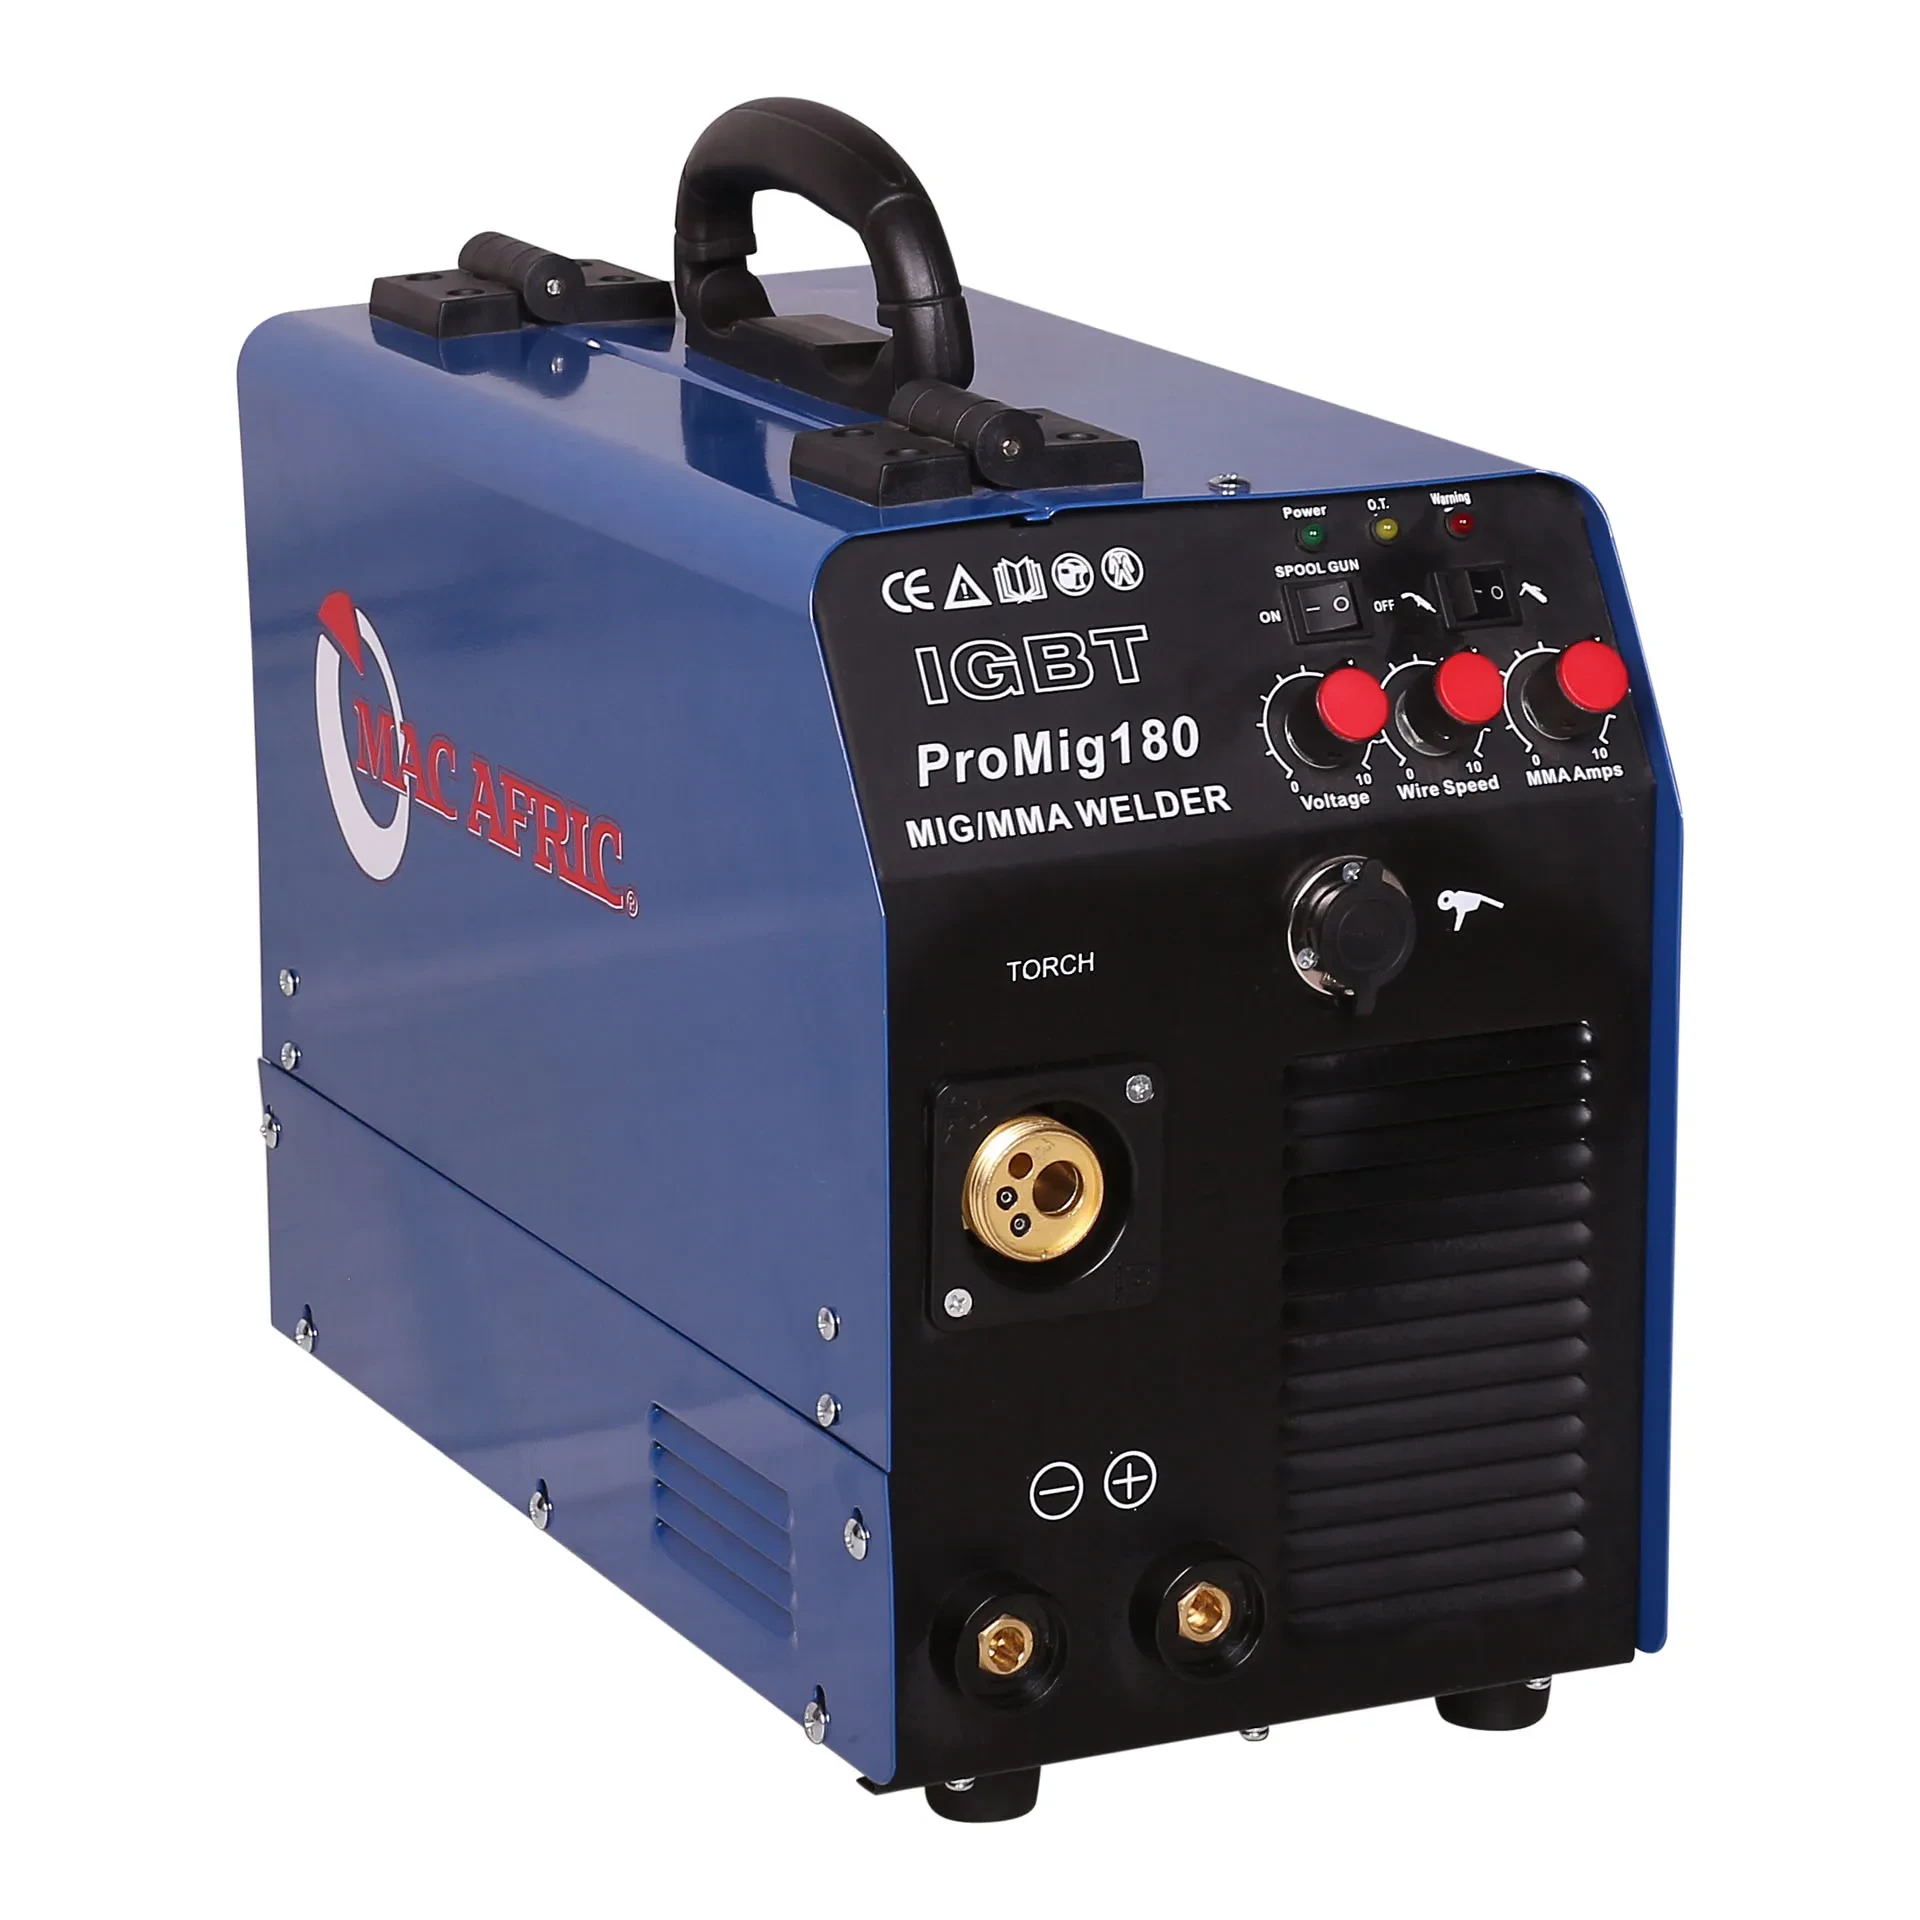
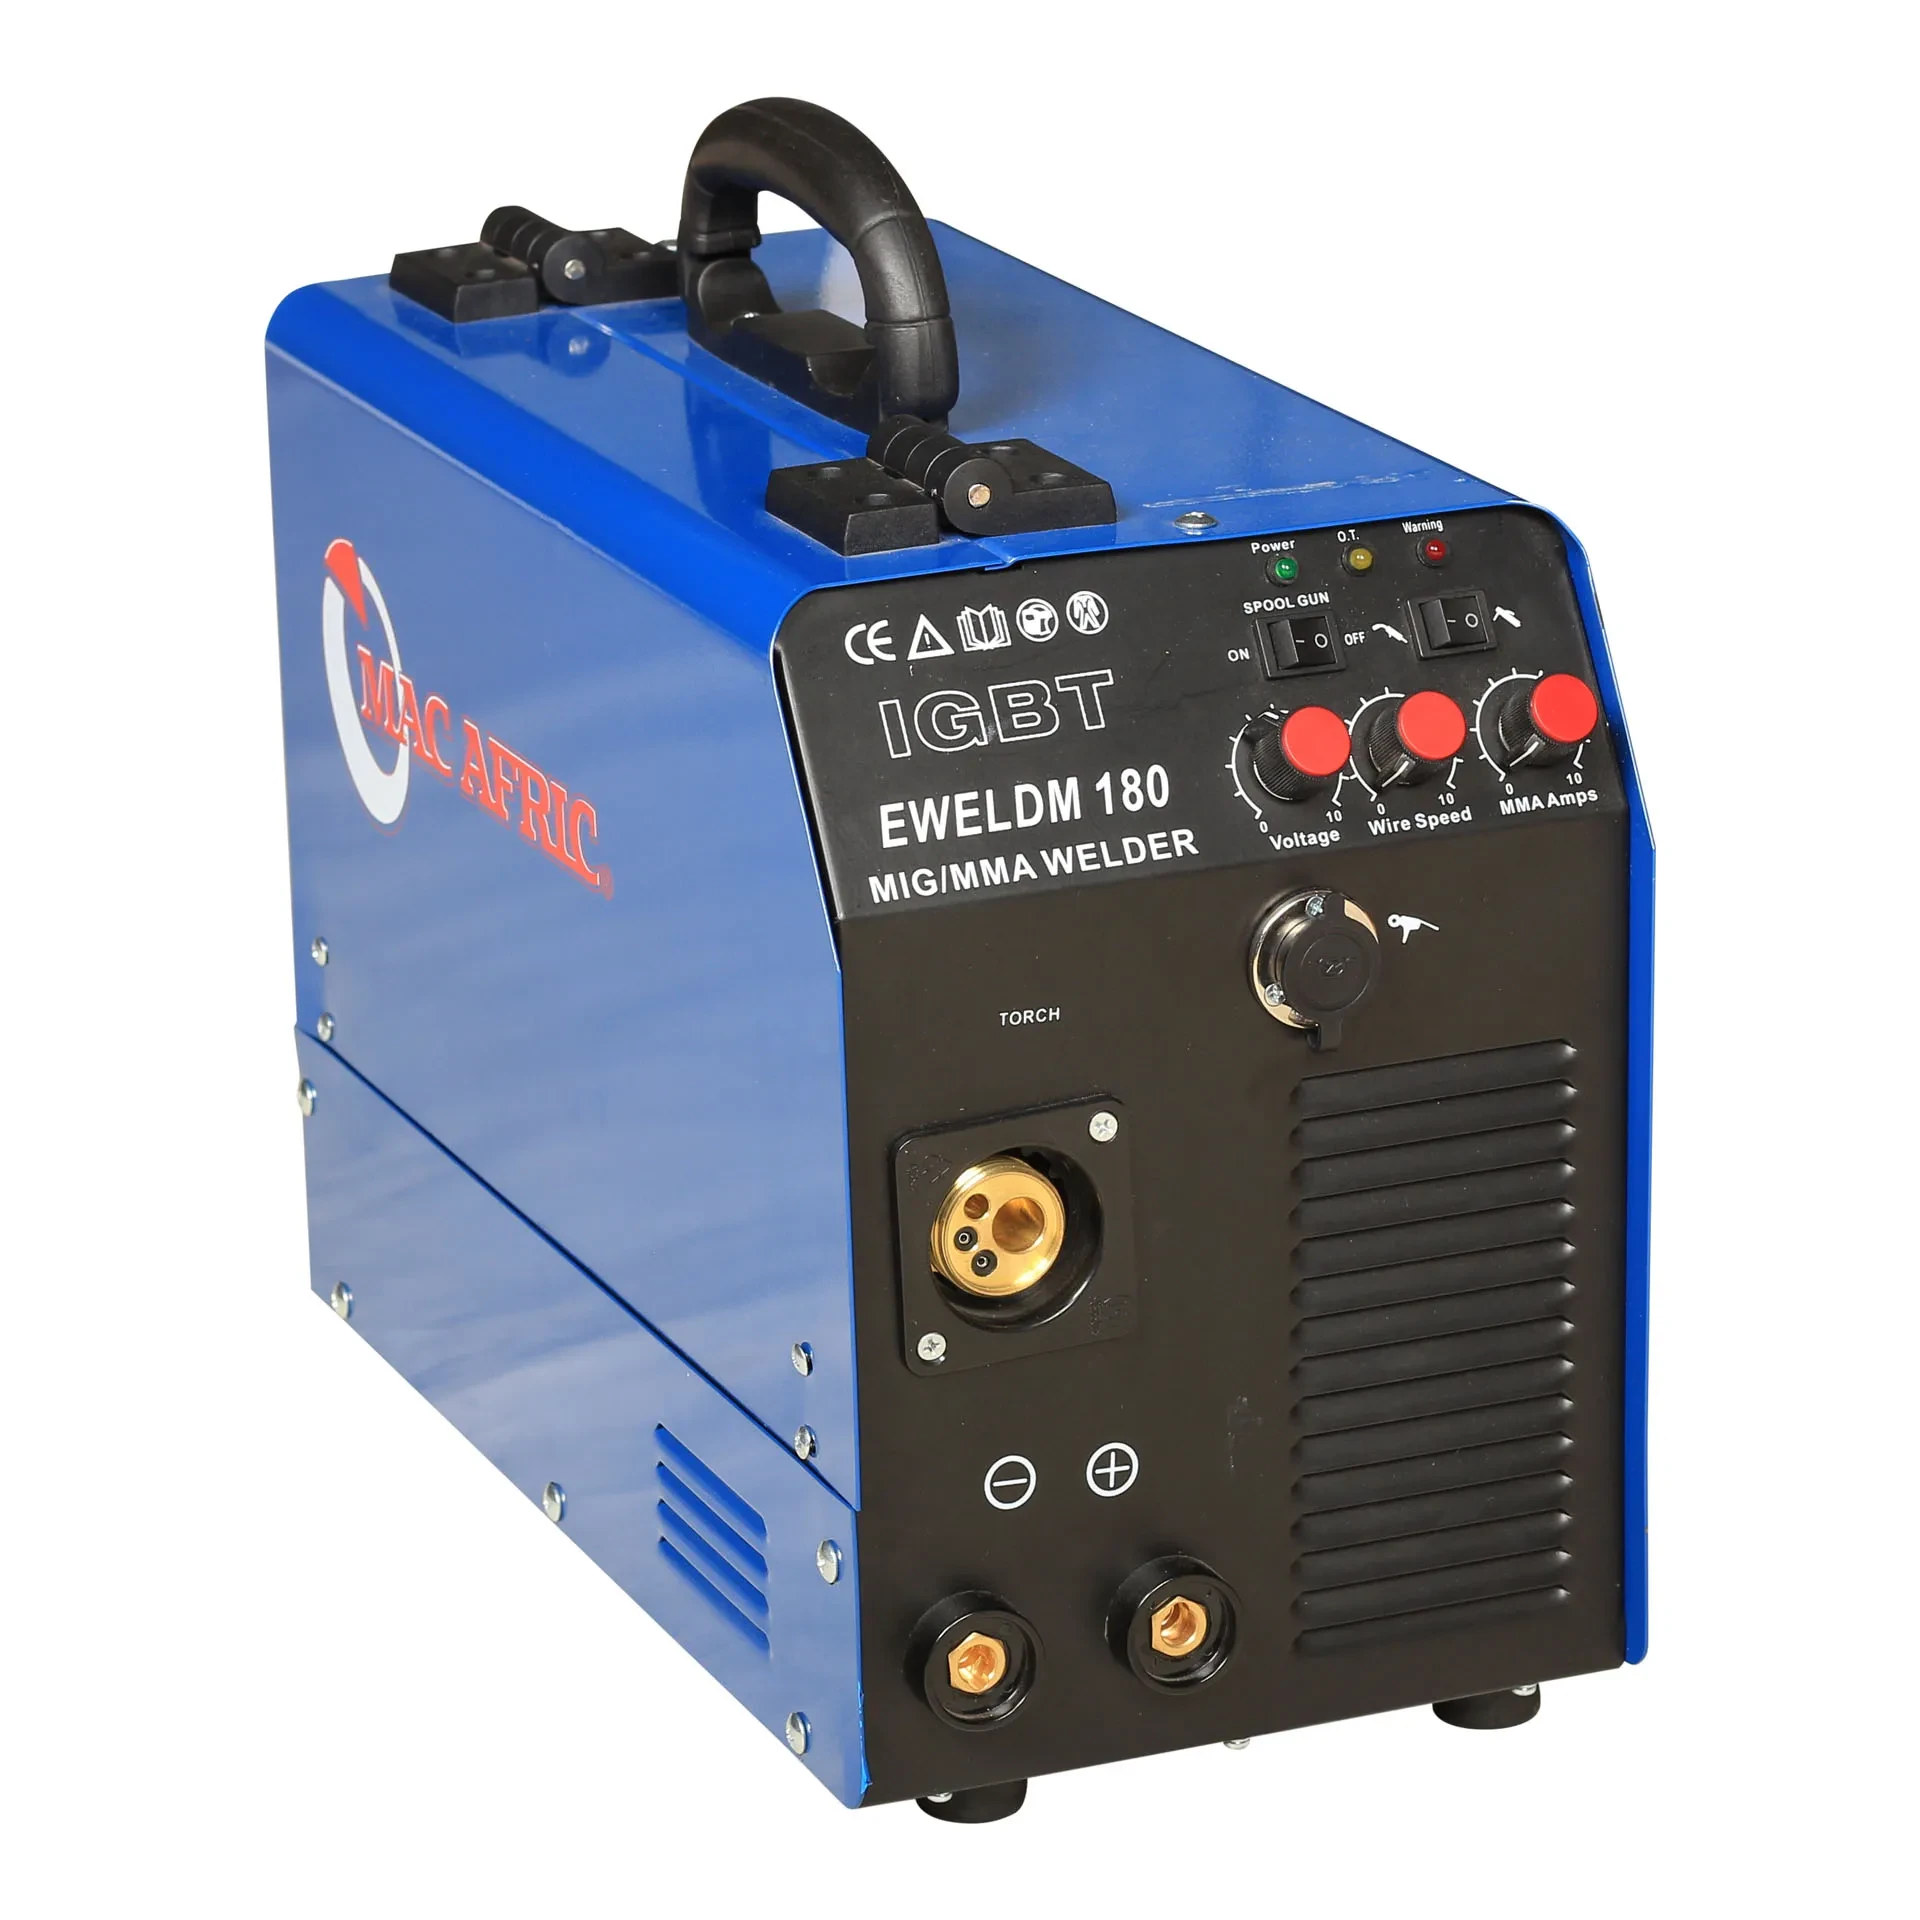
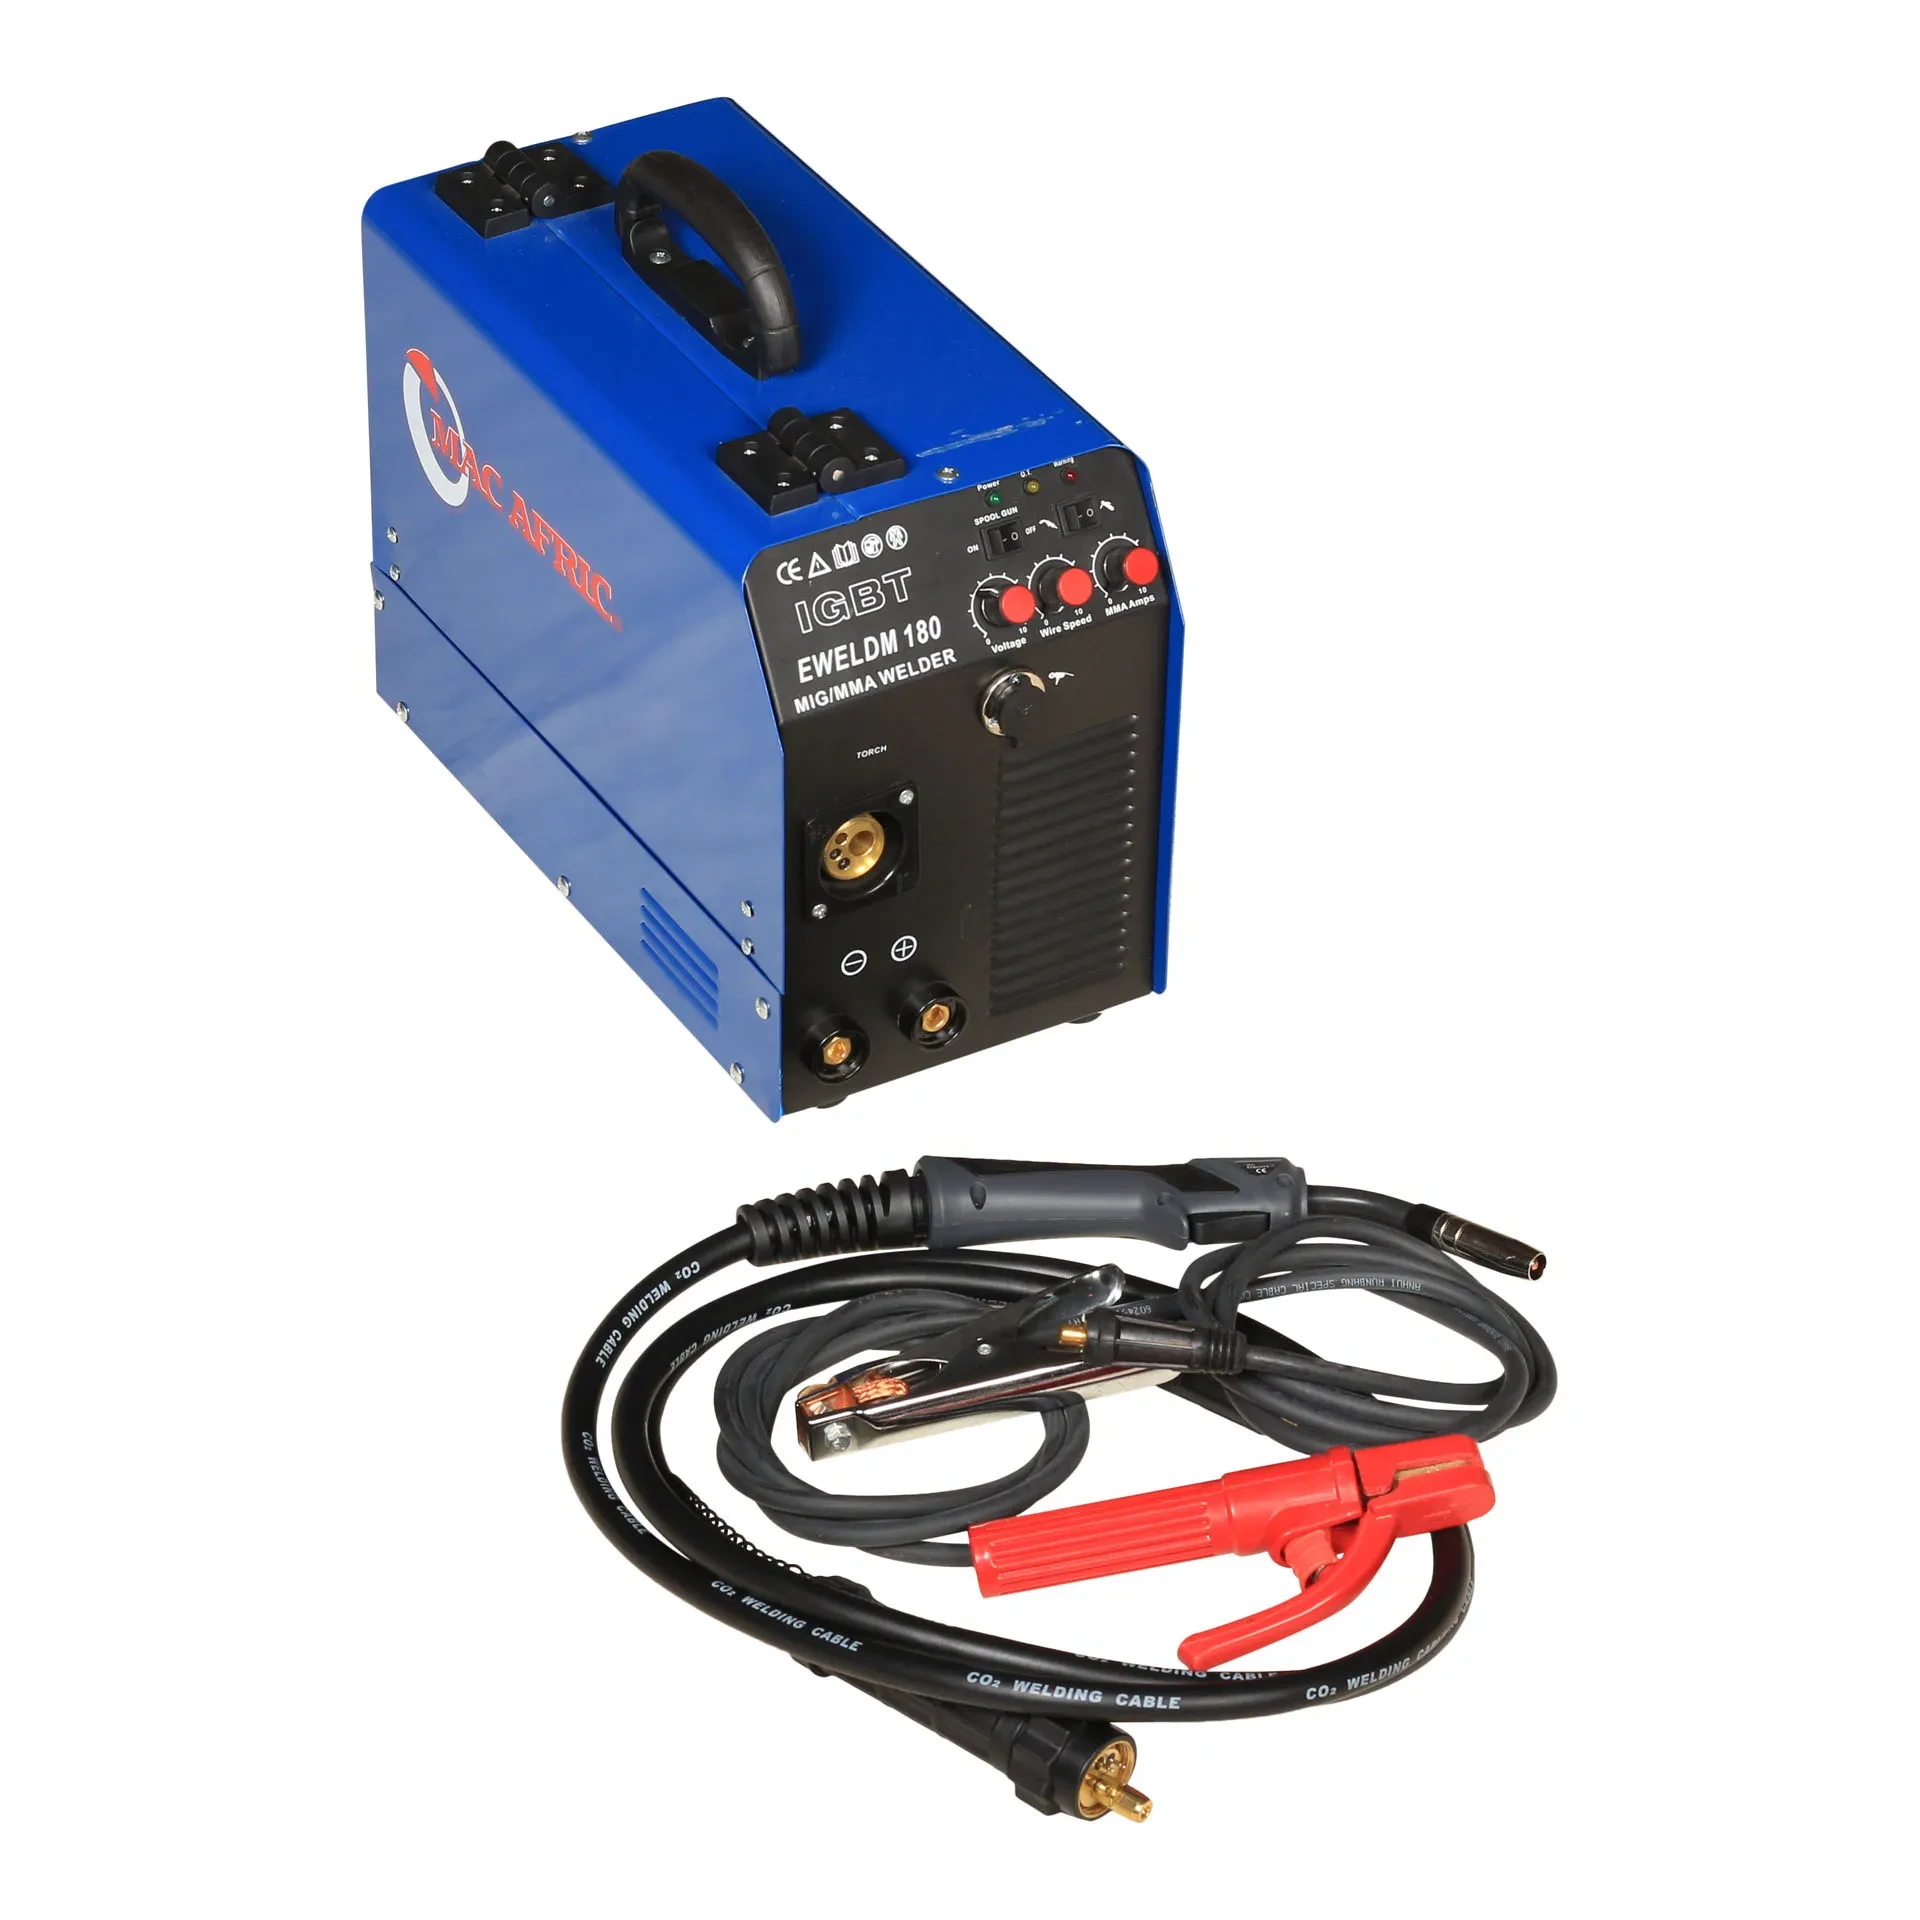
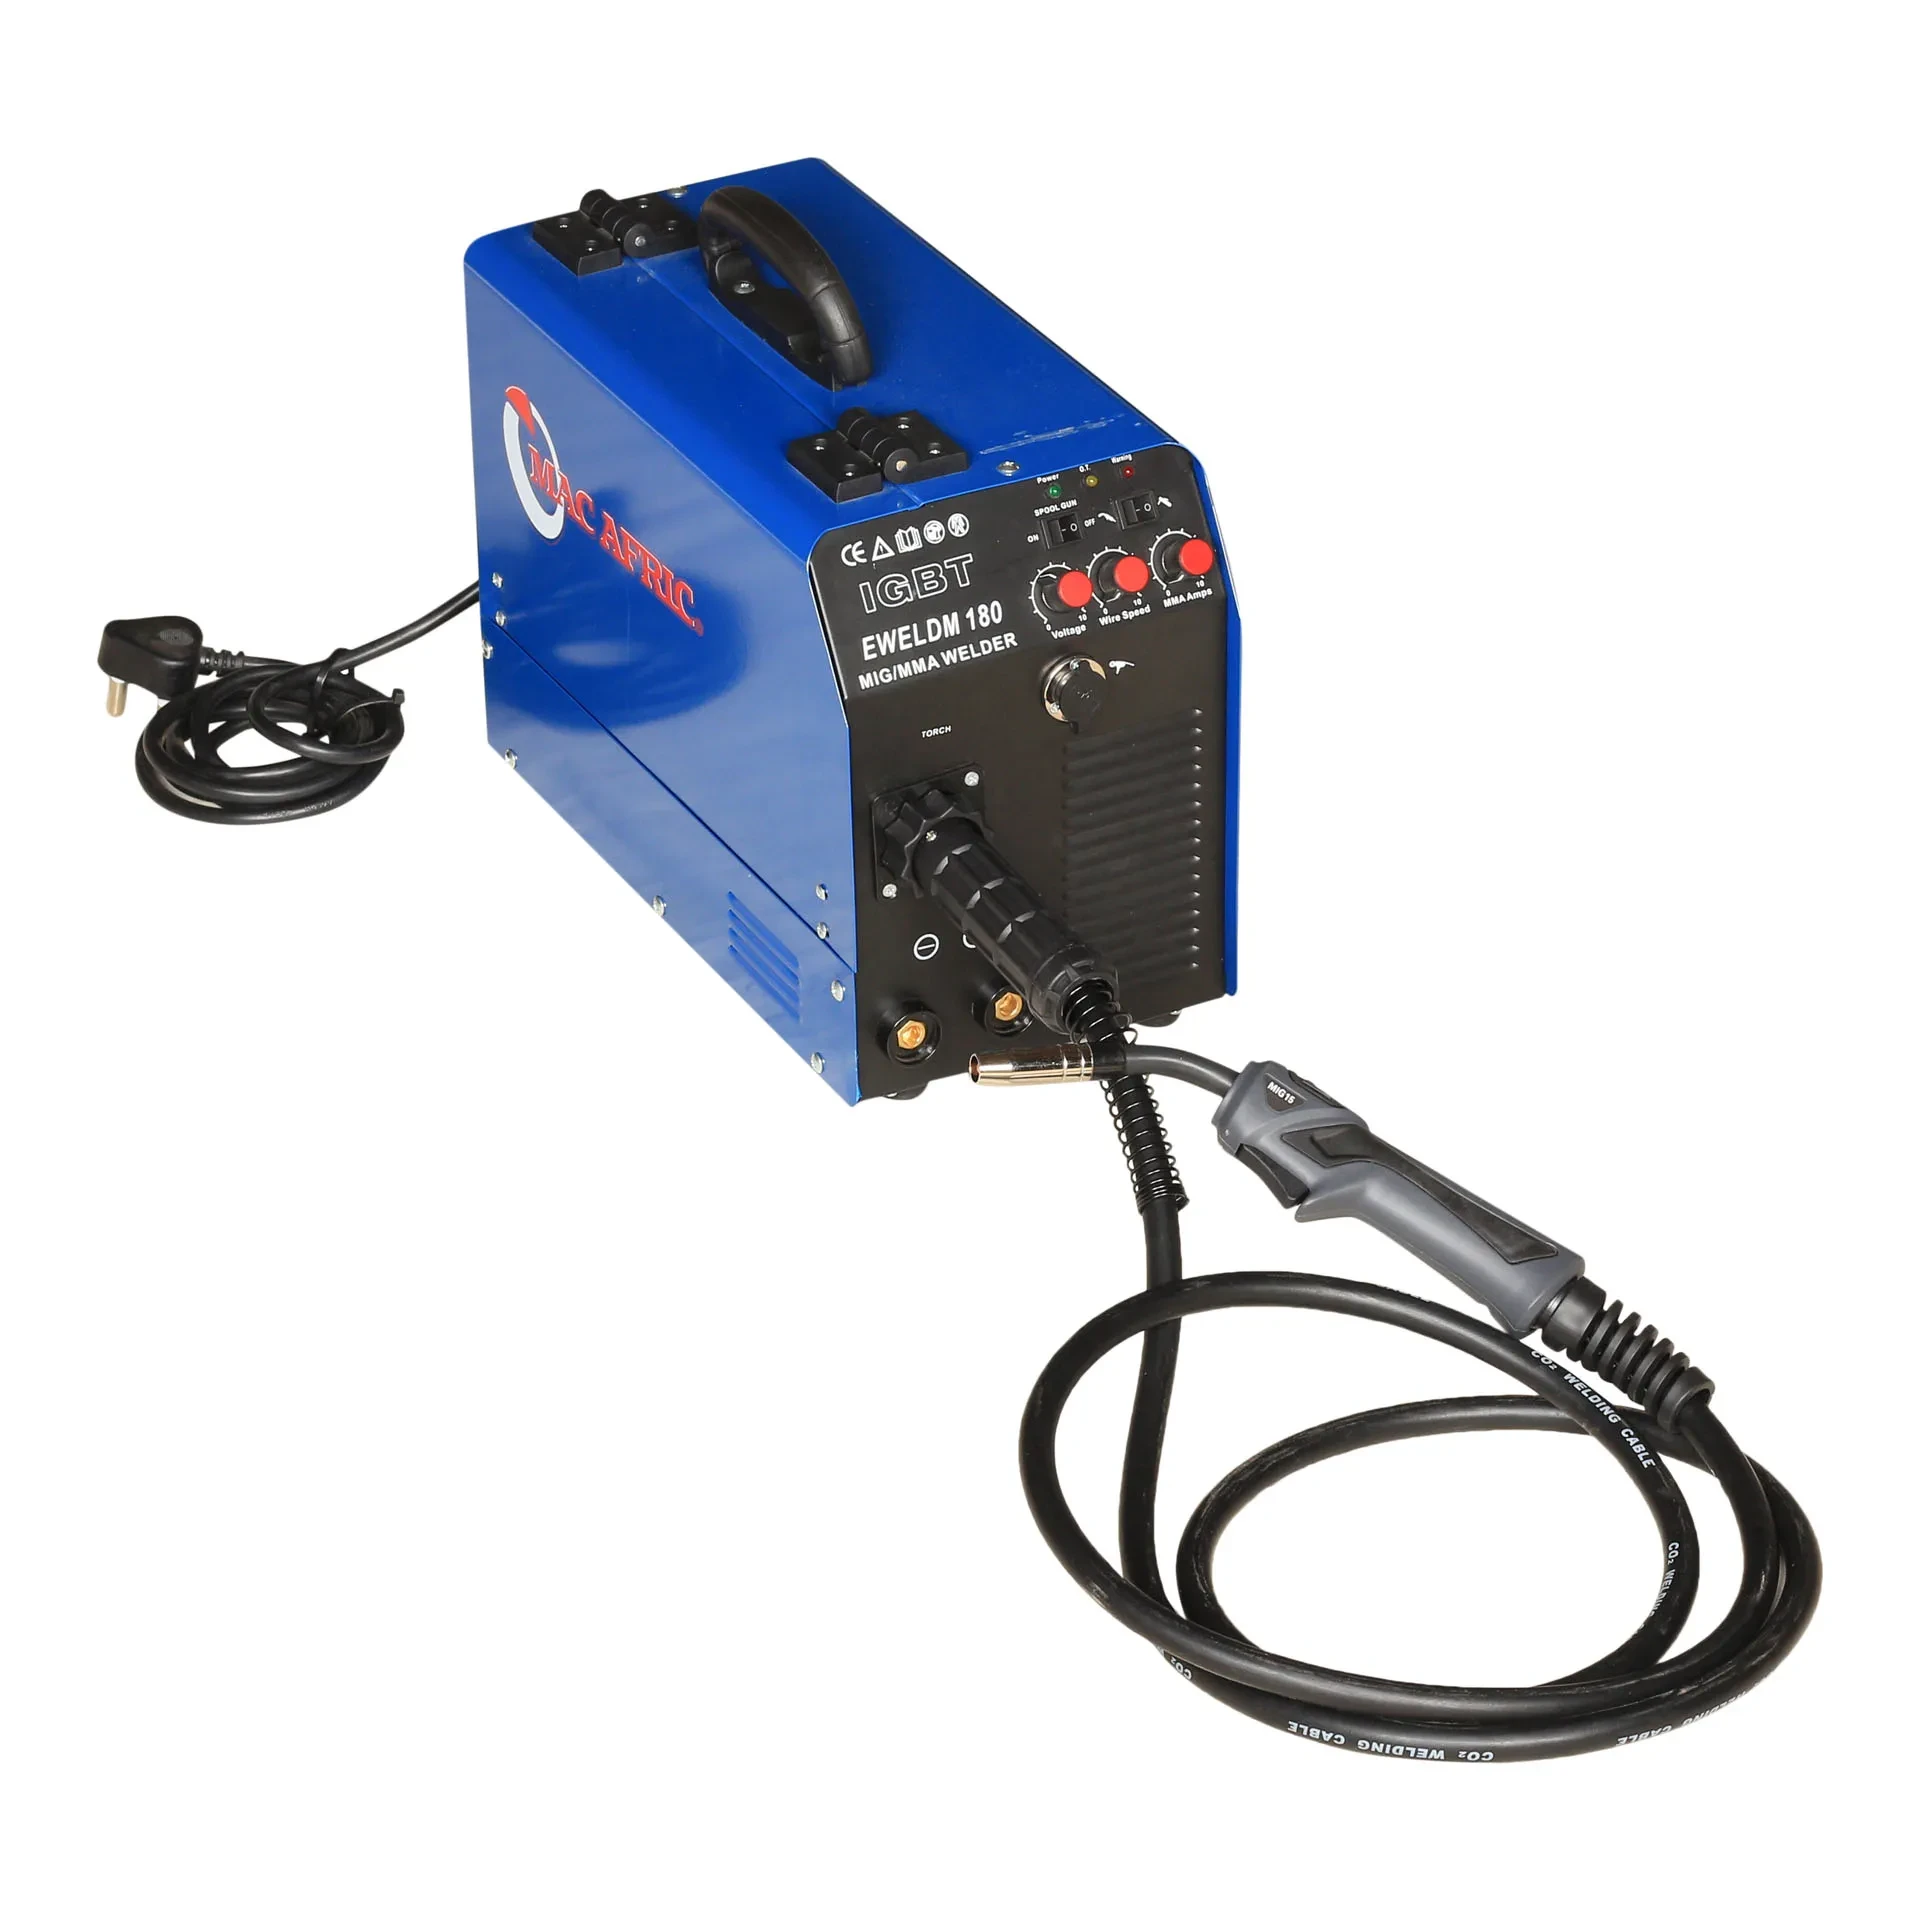
This comprehensive professional 2-in-1 welding machine offers excellent duty cycle and build quality in a smaller, more affordable package. Ideal for both MIG and MMA welding, it combines versatility and efficiency for a wide range of applications.
Technical Specifications
| FeatureSpecification |
|
|
|
| Input Voltage | 230 V @ 50 Hz |
|
|
| Rated Input Current | 30 A |
|
|
| No-Load Voltage | 55 – 75 V |
|
|
| Output Current | 30 – 180 A (MIG / MAG), 15 – 160 A (MMA) |
|
|
| Duty Cycle | 180 A / 23 V @ 35% | 150 A / 21.5 V @ 60% | 120 A / 20 V @ 100% |
| Suitable Wire Diameter | 0.6 mm, 0.8 mm |
|
|
Key Features
- Includes MIG torch and earth clamp
- Supports both MIG and ARC (MMA) welding
- Reliable IGBT technology
- Compact and portable design
- Allows polarity changes for flux-core wire welding
MIG Welding Settings
| MaterialWire TypeWire DiameterVoltageWire SpeedGas TypePolarity |
|
|
|
|
|
|
| Mild Steel | ER70S-6 Solid Wire | 0.8 – 1.0 mm | 16–19 V | 5 – 7 | CO₂ or Argon/CO₂ Mix | DCEP (+) |
| Stainless Steel | ER308L Solid Wire | 0.8 – 1.0 mm | 18–20 V | 5 – 6.5 | 98% Argon + 2% CO₂ | DCEP (+) |
| Galvanised Steel | ER70S-6 Solid Wire | 0.8 mm | 15–18 V | 5 – 6 | CO₂ or Argon/CO₂ Mix | DCEP (+) |
MMA (Stick) Welding Settings
| MaterialElectrode TypeRod SizeAmperagePolarityNotes |
|
|
|
|
|
| Mild Steel | E6013 | 2.5 mm | 90 – 100 A | DCEP (+) | All-position, easy to use |
| Mild Steel | E6013 | 3.2 mm | 110 – 125 A | DCEP (+) | For thicker steel |
| Stainless Steel | E308L-16 | 2.5 mm | 85 – 100 A | DCEP (+) | For tanks and pipes |
| Cast Iron | E7018 / ENiFe-CI | 3.2 mm | 100 – 120 A | DCEP (+) | Preheat recommended |
Spool Gun Setup (Optional for Aluminium)
| MaterialWire TypeWire SizeVoltageWire SpeedGas TypePolarityNotes |
|
|
|
|
|
|
|
| Aluminium | ER4043 / ER5356 | 1.0 mm | 18–22 V | 6 – 8 | 100% Argon | DCEP (+) | Use spool gun mode; keep cable straight |
Setup Tips
- Always use clean and dry wire or rods
- Use proper drive rollers for MIG
- Clamp on bare, clean metal for MMA
- Shield from wind when using gas
- Avoid exceeding 5–6 minutes continuous weld at high amps
Troubleshooting FAQ
| IssueLikely CauseRecommended FixPro Tip |
|
|
|
| No arc | Loose clamp, low amps | Clamp to clean metal, increase amps | Always ground to bare, unpainted metal |
| Electrode sticks | Low amps, dirty metal | Use 90–100A, clean surface | Use E6013 for easy restarts |
| Arc pops or cuts out | Loose terminal, poor rod angle | Tighten cables, use correct angle | Store rods in sealed container |
| Breaker trips | Overload or poor socket | Use 20A+ socket, rest machine | Never use long extensions |
| Turns on but no weld | Blown fuse or PCB fault | Check lights, get technician check | Use surge protector |
| Weak weld | Low amps, wrong polarity | Use 90–125A, correct polarity | Keep consistent bead speed |
| Excessive spatter | Long arc, dirty base | Shorten arc, clean metal | 15° rod angle helps |
| Overheat light | Overuse beyond duty cycle | Rest 10–15 min, lower output | Use in shaded, ventilated area |

 English
 English